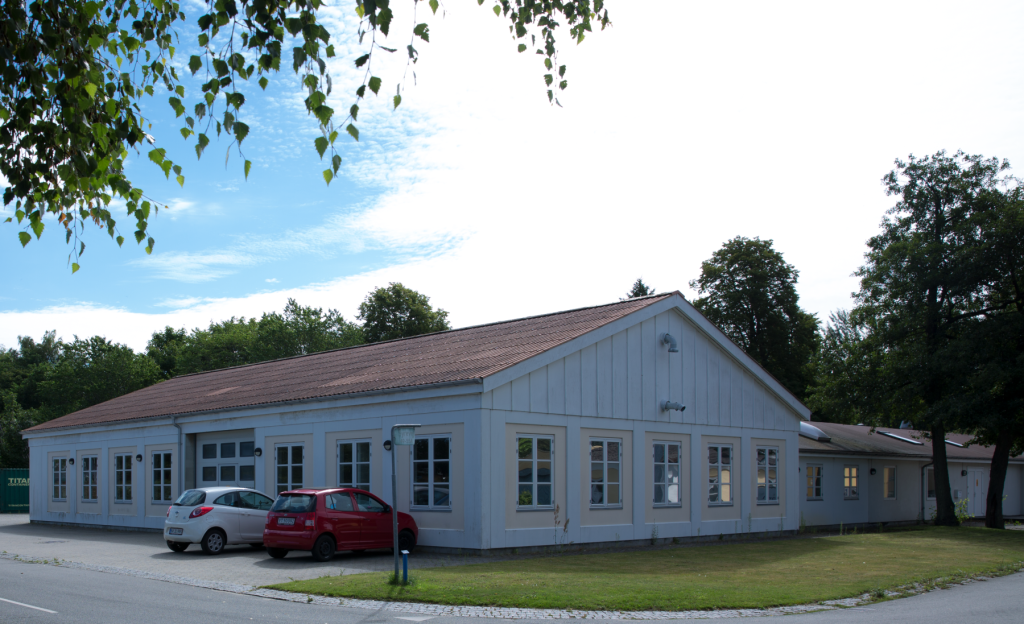
produced in an FDA-registered facility
Quality control.
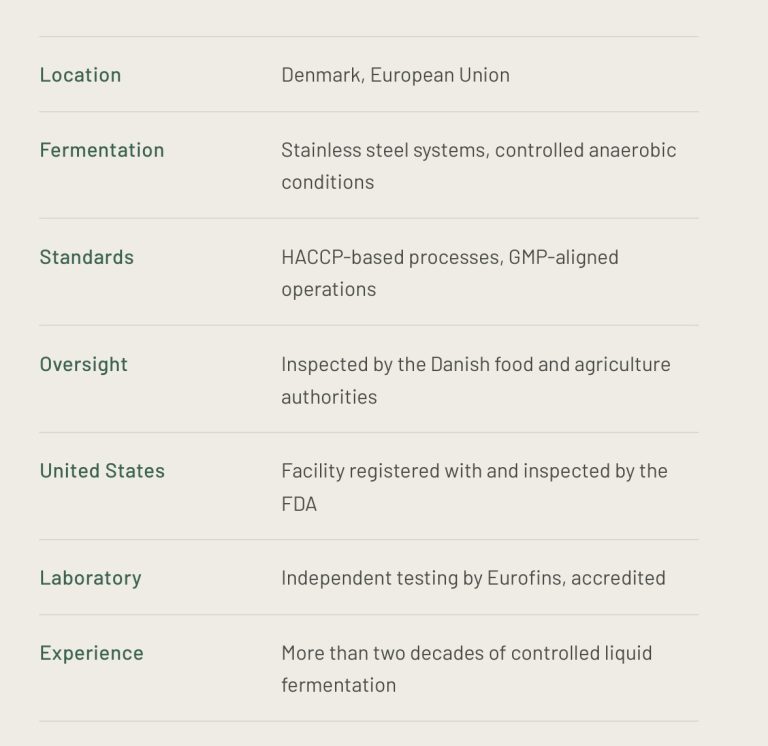
Every batch is fermented, tested, filled and released in our own facility in Denmark. Under HACCP, organic certification and continuous inspection by the Danish food authorities.
Control starts long before
the fermentation tank
Postbiotics are only as consistent as the process that produces them. Ours runs end to end in one place: certified organic botanicals in at one door, a documented and released ingredient out at the other.
A defined blend of certified organic botanicals and eight selected bacterial strains, fermented under anaerobic conditions over an extended period, until the sugars from the organic cane molasses are converted to below the detection limit.
The pH settles at approximately 3.3, which makes the product self preserving. Nothing synthetic is added and there is no heat treatment afterwards, so the fermentation-derived compounds reach you as they were formed.
For a formulator that means a defined ingredient, batch after batch, with the documentation to prove it
— 24 months shelf life at room temperature, no cold chain.
From organic herbs
to a released batch.
01. Raw materials
A defined blend of certified organic botanicals, organic cane molasses, water and eight selected bacterial strains. Suppliers are registered and re-evaluated at a fixed frequency within the quality management
system, and every incoming lot is documented before it is released to production.
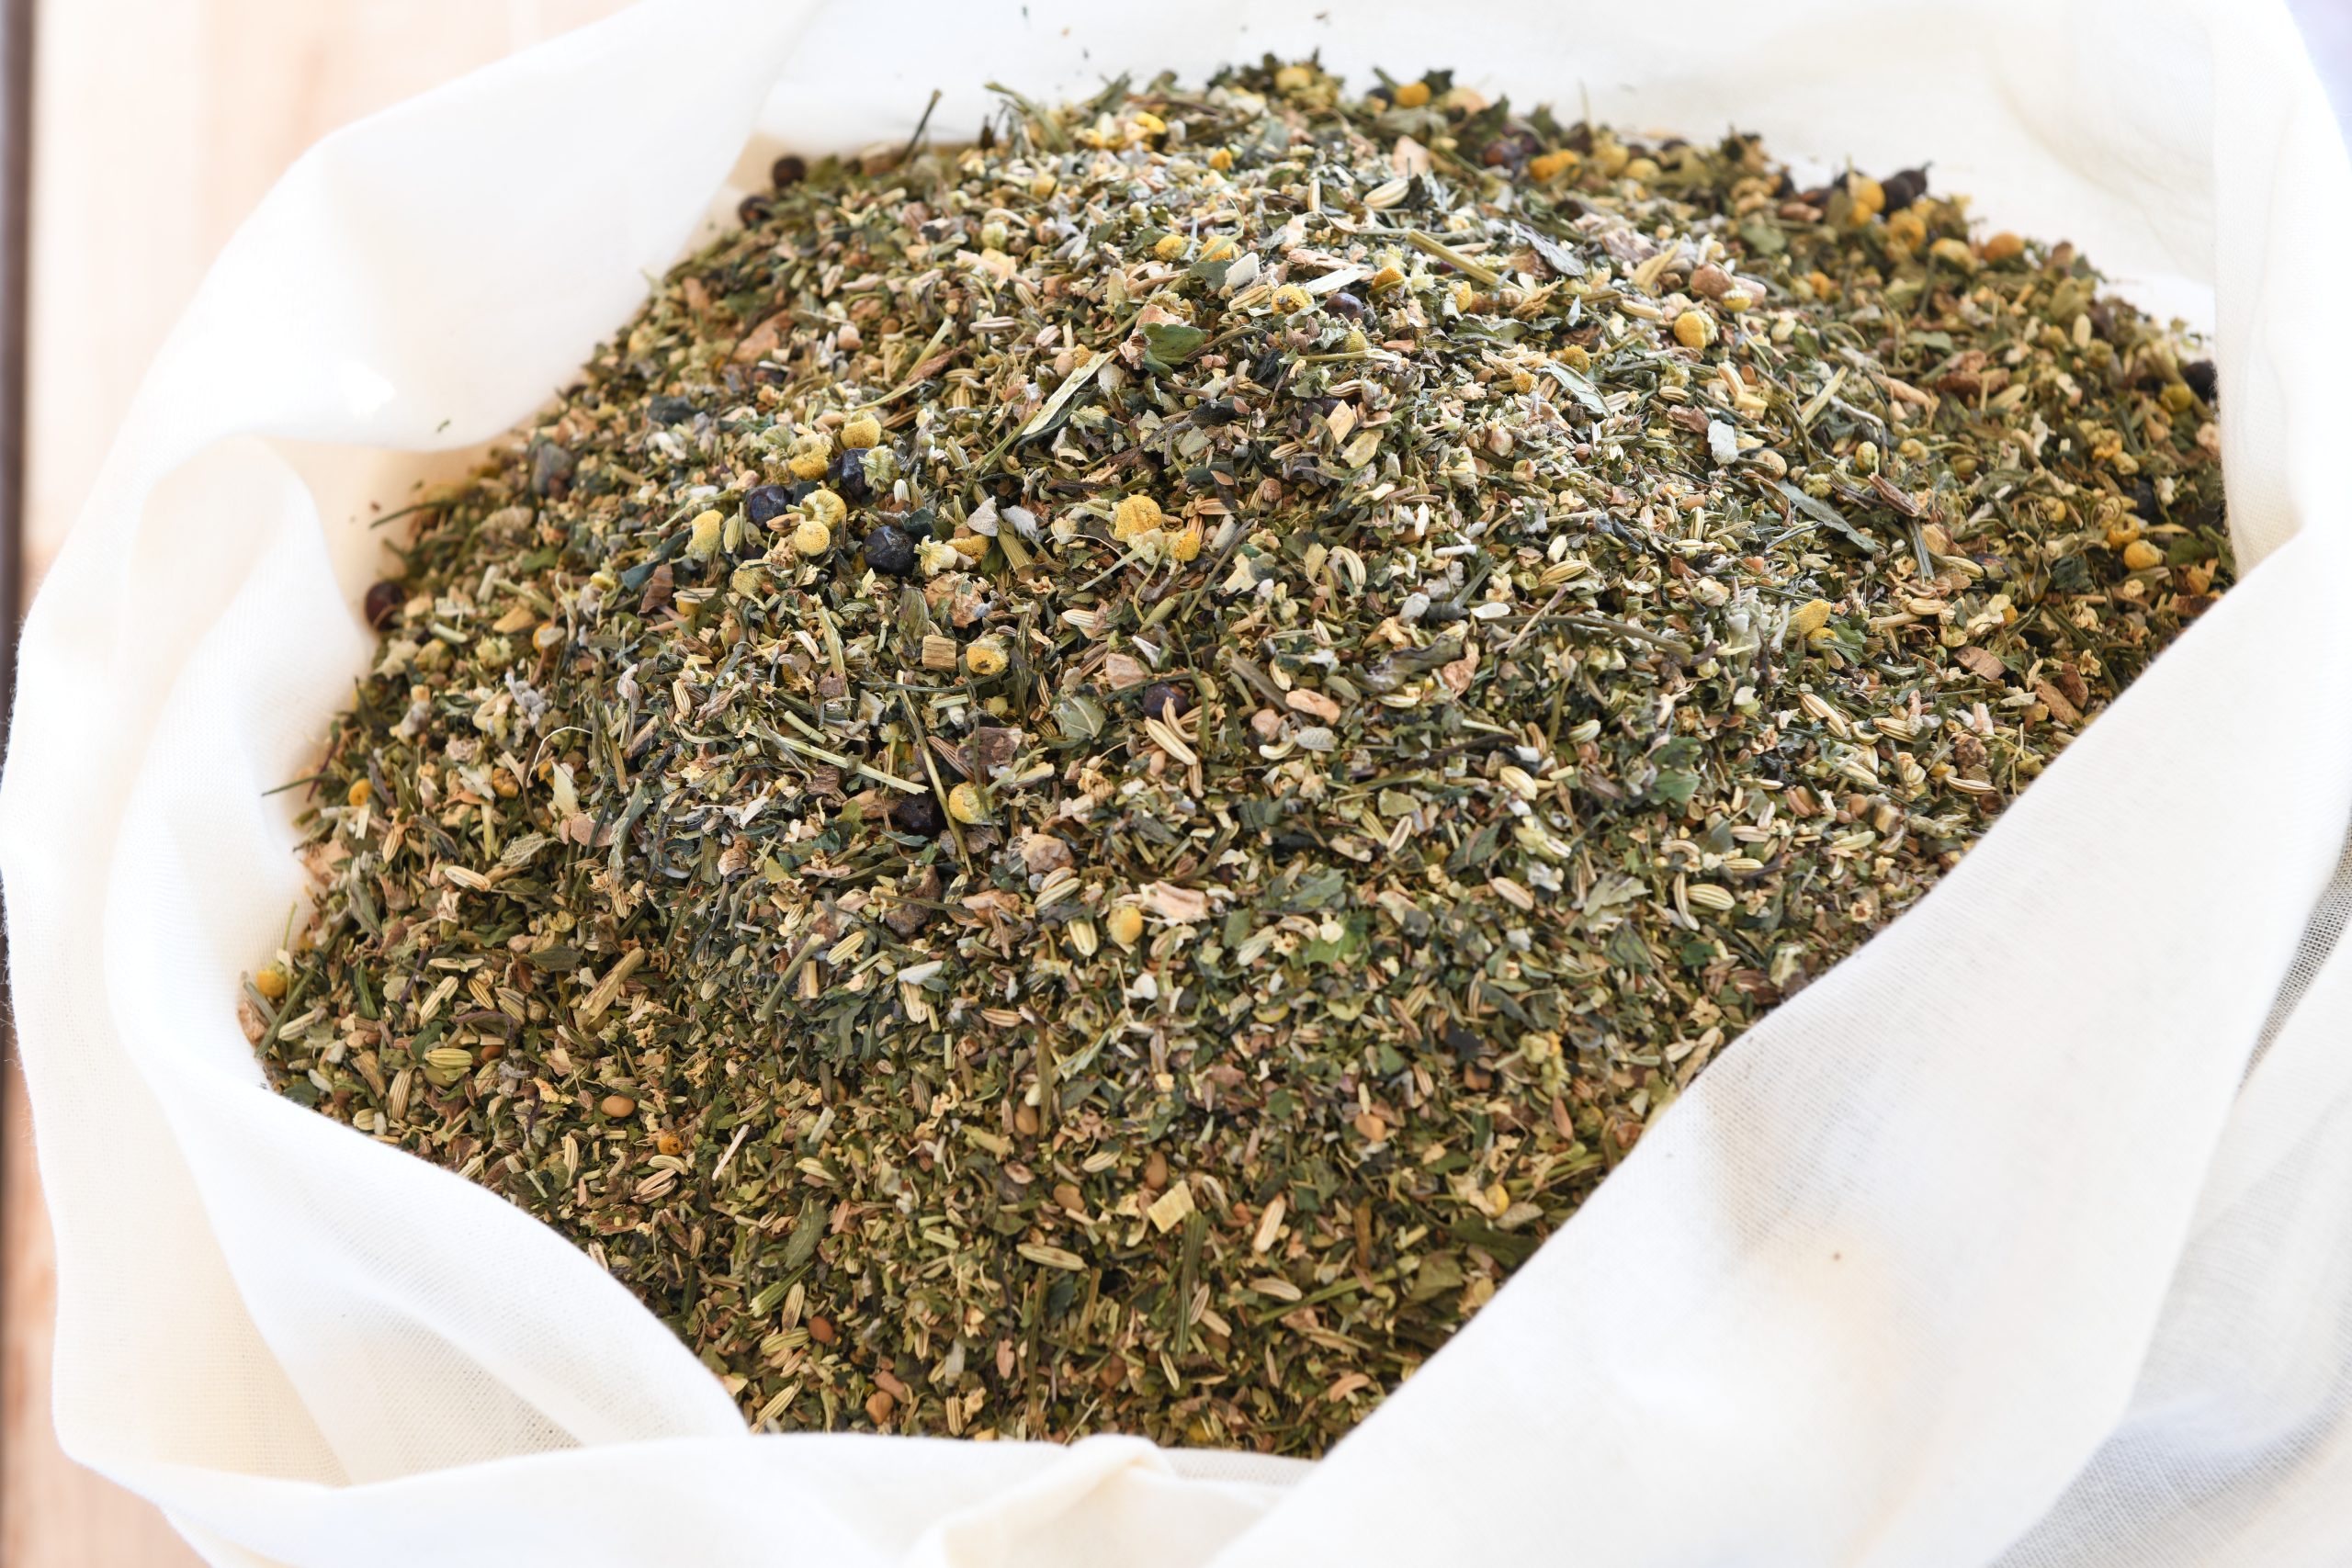
Botanicals include aniseed, fennel seed, liquorice root, angelica root, camomile,
elderflower, juniper berry, nettle, peppermint, rosemary, sage and thyme.
The full composition is shared with partners under NDA
02. Controlled fermentation
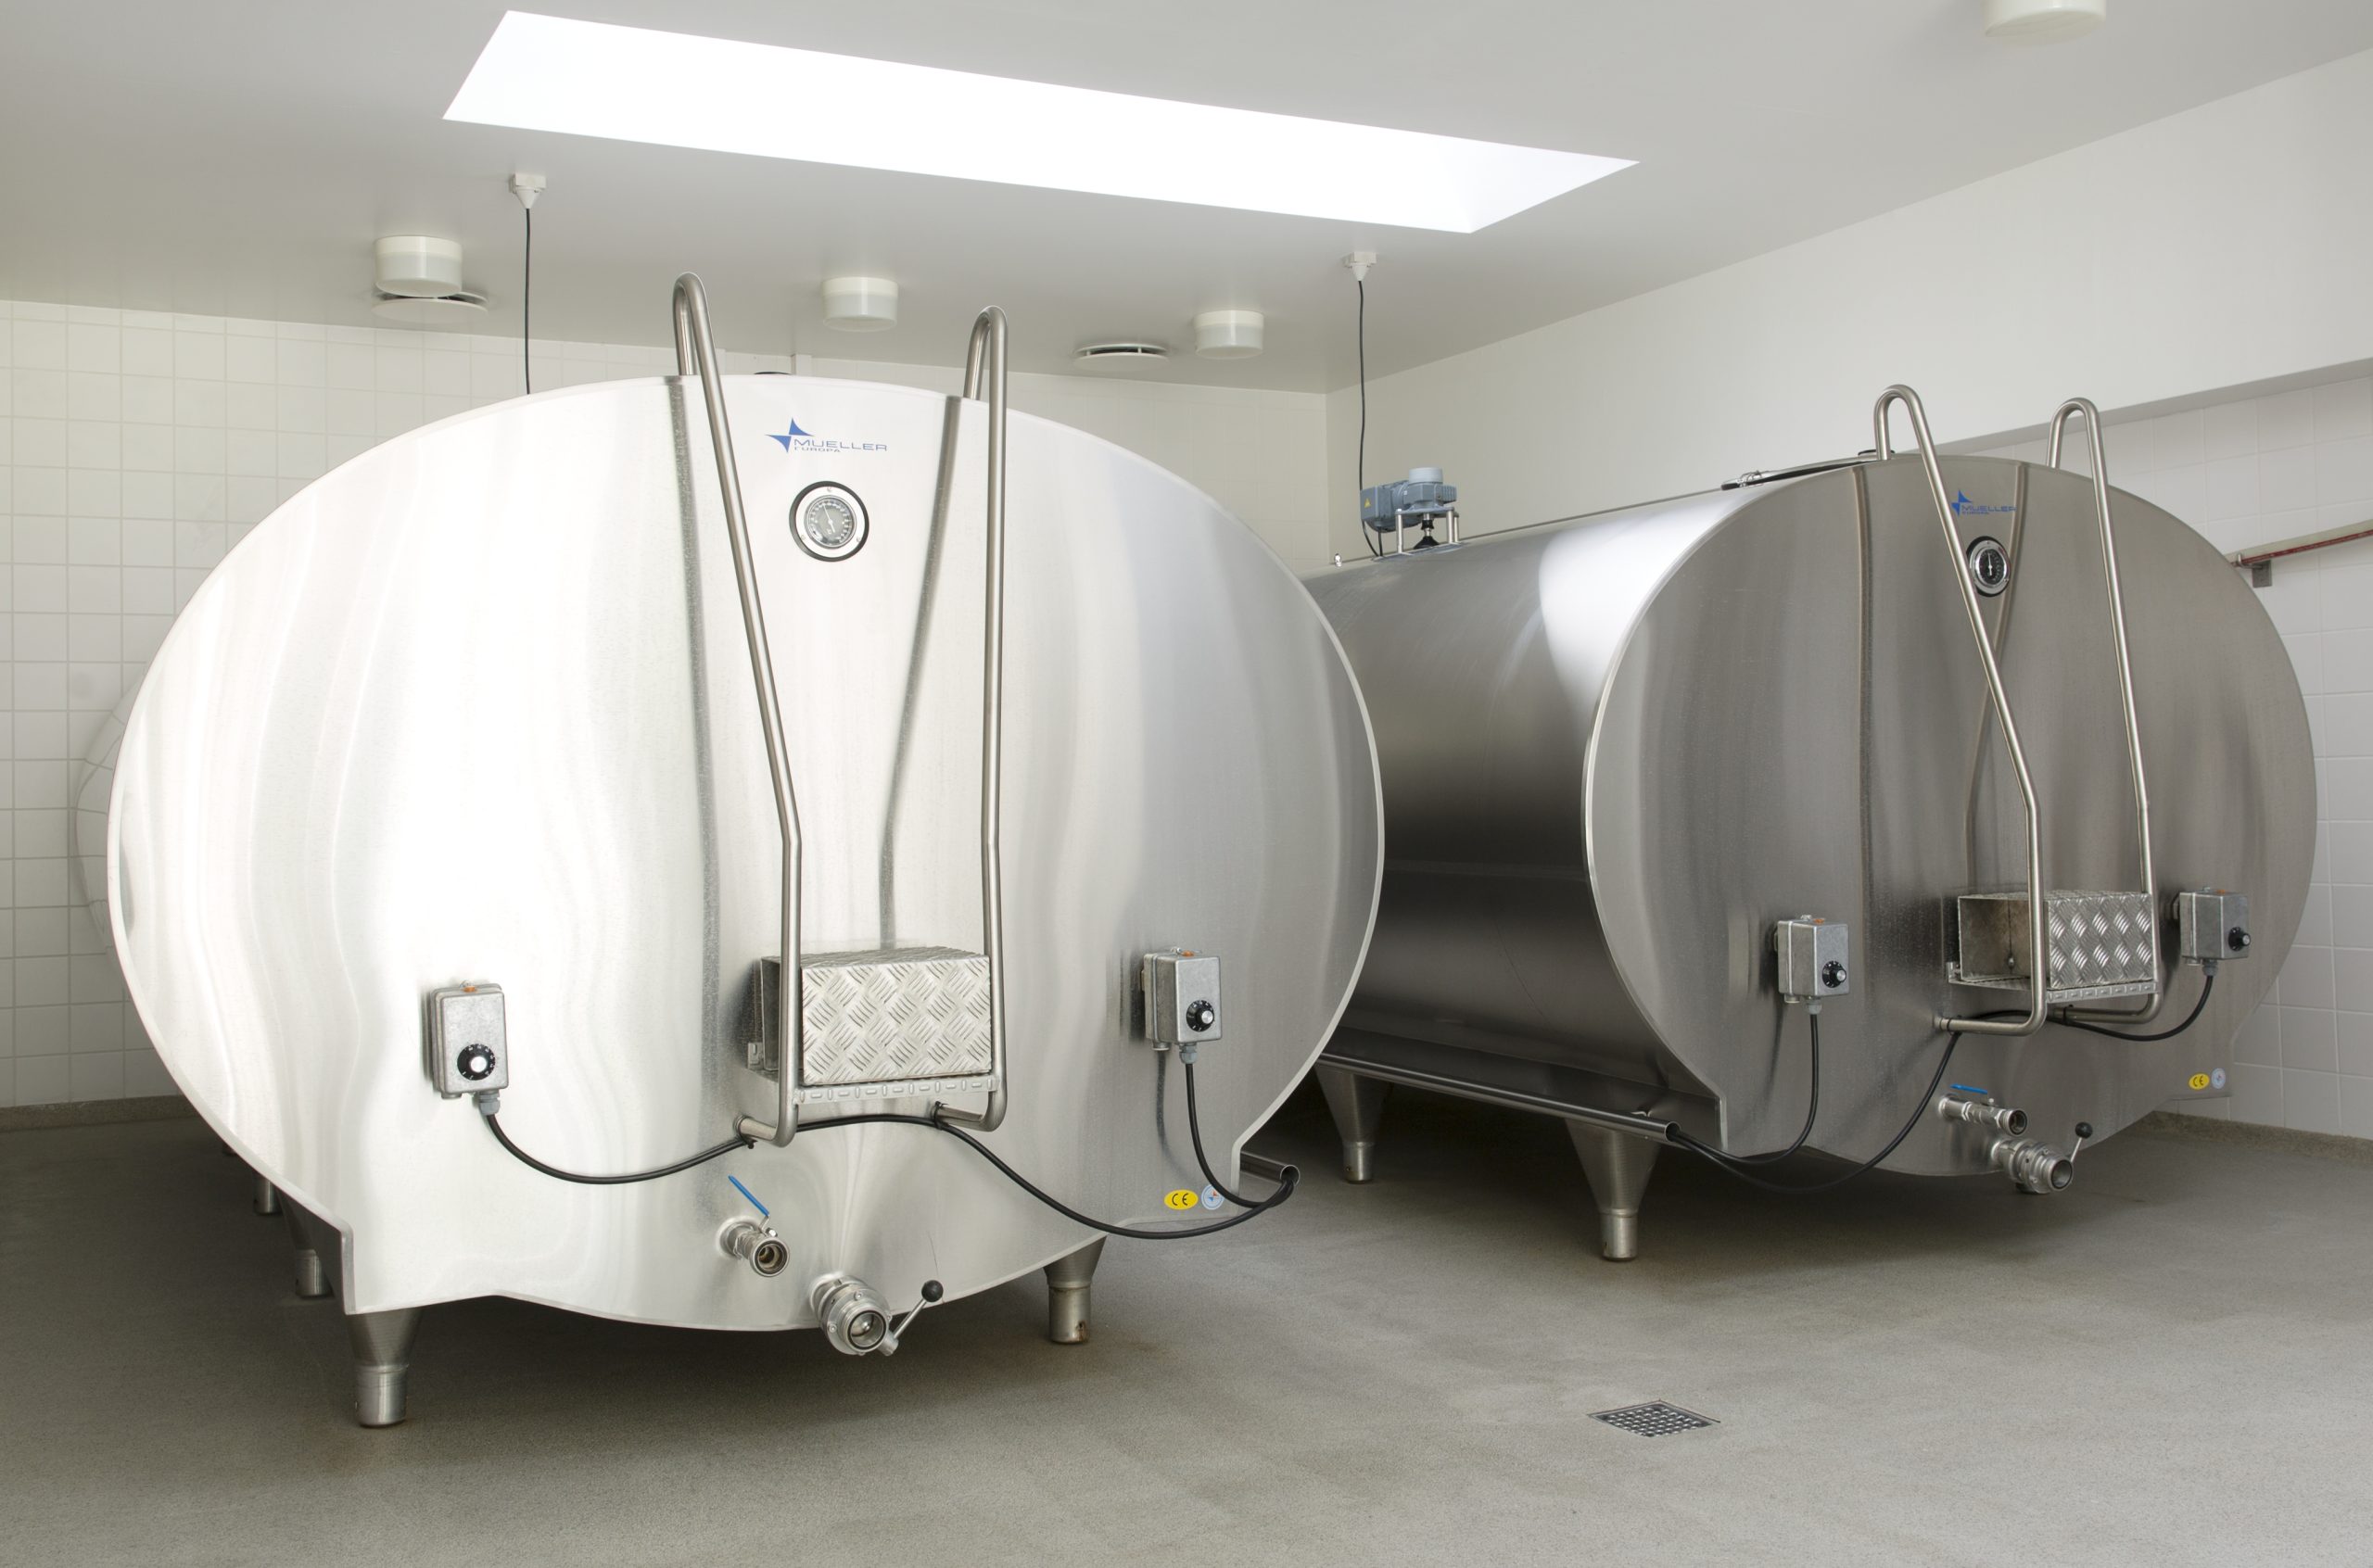
Fermentation takes place in stainless steel systems under controlled anaerobic conditions and defined temperature, and continues for as long as the process requires.
Microorganisms convert the carbohydrates into organic acids and other metabolites; the solid plant material is drawn off, so what remains is the extract.
pH is monitored throughout and stabilises at approximately 3.3.
There is no post-fermentation heat step, and no preservatives or excipients are used.
03. Filling and packaging
Only a fully released batch is allowed to proceed to the production line.
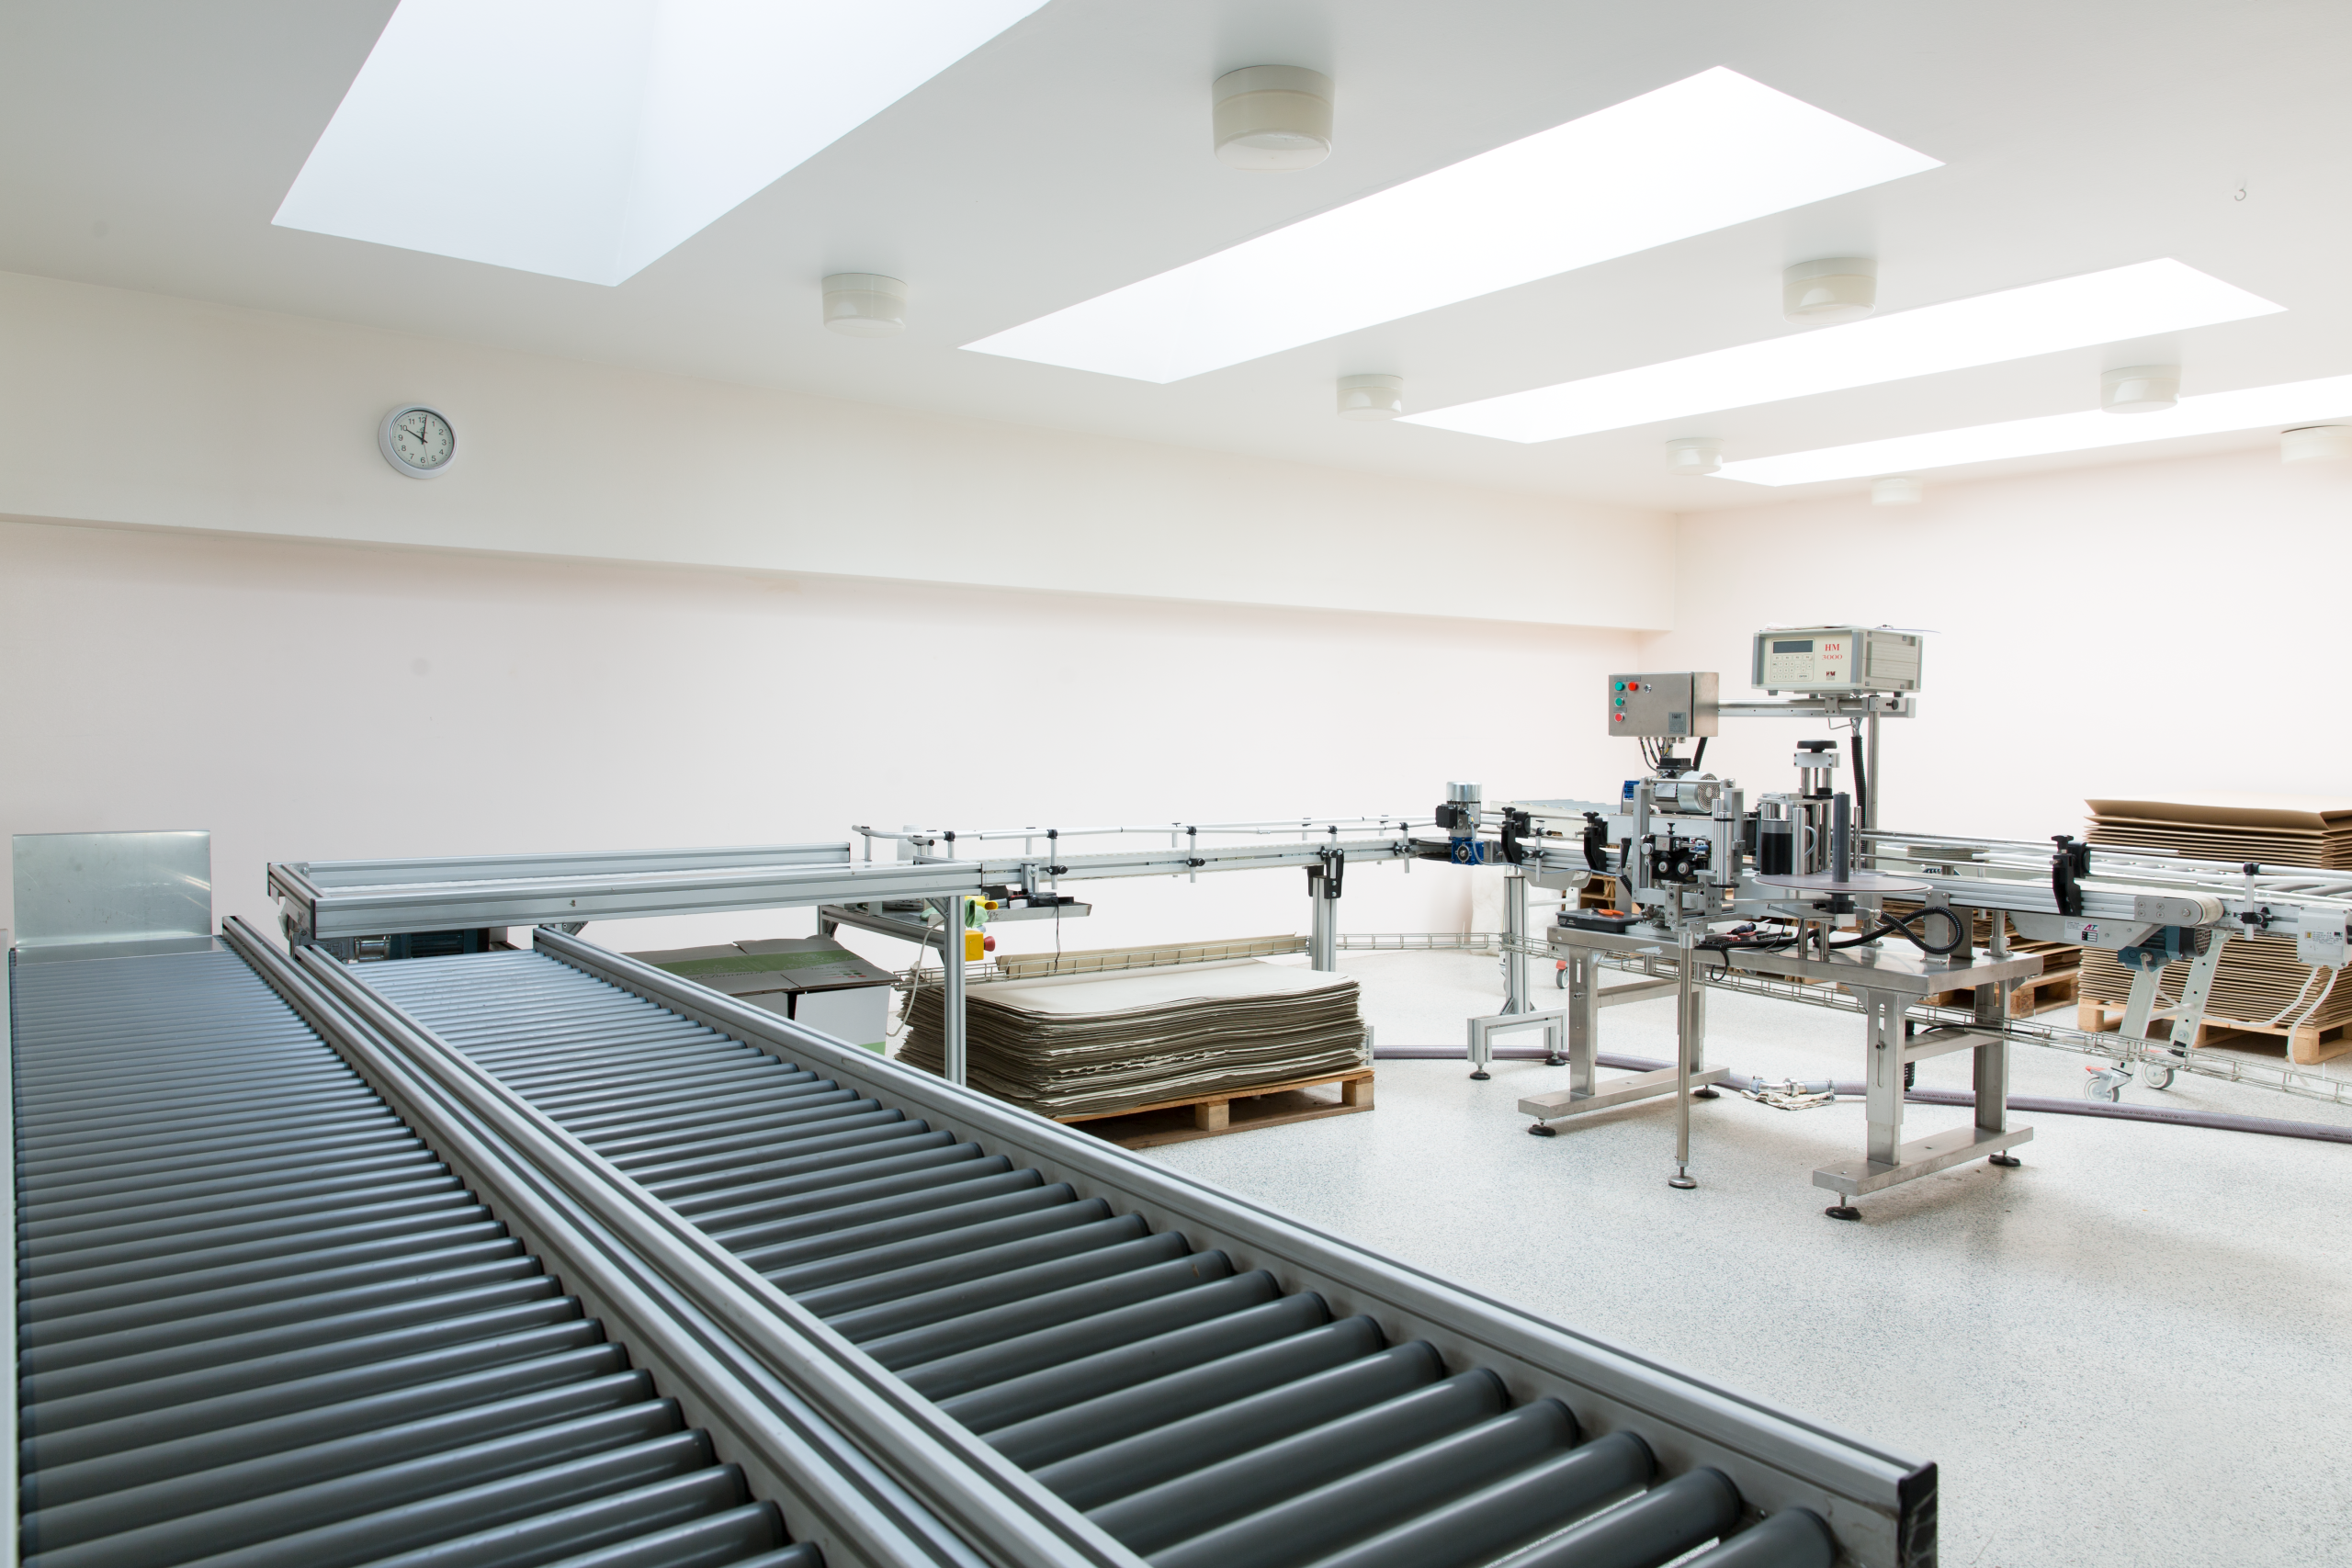
Our filling and labelling operations are carried out entirely in-house, giving us full control over the process from the moment a batch is approved through to the final packaged product. We can accommodate a wide range of formats and volumes, from 500 ml bottles for finished consumer products to 1,000-litre IBCs for bulk applications.
Regardless of the final format, the same quality standards, procedures and controls apply throughout the entire process.
Tested in process
and tested again at the end.
Quality is verified by our own controls and by independent accredited laboratories. Nothing leaves the facility without documentation.

Fermentation, testing, filling and packing happen under a single roof and a single quality system, which is what makes batch-to batch consistency a process outcome rather than a promise. Partners with a QA team are welcome to audit it, or to walk it.
Certified where it counts.
Organic certification
Raw materials and production are covered by organic certification under Danish state control.
HACCP
Production and quality systems built on HACCP principles and EU food safety legislation.
FDA-registered facility
Registered with and inspected by the US Food and Drug Administration. Registration details on request.
Non-GMO and vegan
No GMO inputs, no animal ingredients, and no animal testing in development or production.
Accredited laboratory
Independent analysis by Eurofins, with a Certificate of Analysis available per batch.
Regulatory support
Guidance on documentation and market requirements for the application you are building.
Audit the process
not just the datasheet.
Request the production and quality dossier, ask for samples with the matching batch documentation, or bring your QA team to the facility.